
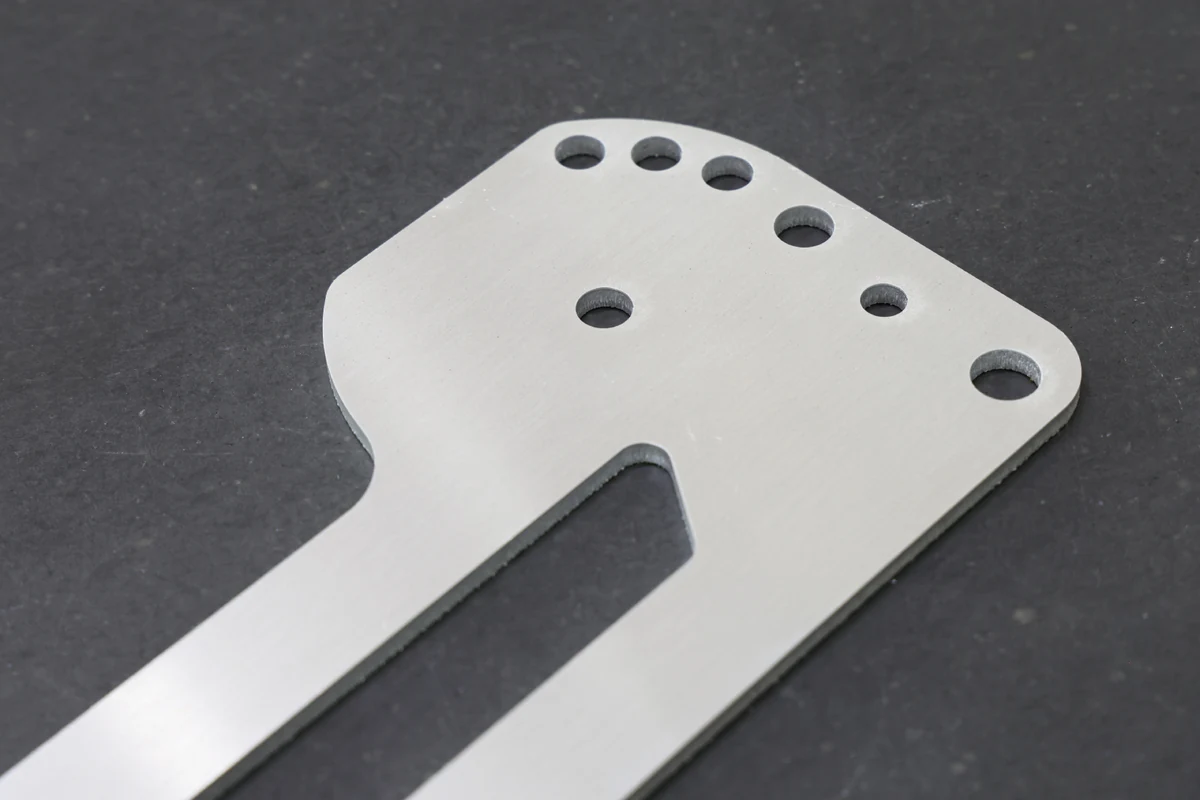
- Key Takeaways
- How to Prepare a Design File for Laser Cutting
- What Are the Design Rules for Laser Cut Parts?
- How Do You Choose the Right Material for a Laser Cut Part?
- What Tolerances Apply for Laser Cutting?
- What Affects the Cost of a Laser Cut Part?
- DFM Checklist
- FAQ
The design rules for laser cut parts are mainly based on the sheet’s thickness (T) and some numbers that scale directly with it.
The main DFM rules to follow are:
- Keeping hole diameter to a minimum of 0.6×T and spacing holes at least 2×T from all edges and 5×T from each other.
- Ensuring inside corners have a minimum radius of 0.5×T.
- Keeping holes at least 2×T plus the bend radius away from any bend.
- Sending your design as a 3D model, not a 2D drawing of your part.
If you get all these things right, chances are your design will pass the DFM check without needing revisions. Standard laser cutting tolerance is ±0.45 mm on linear dimensions and ±0.12 mm on hole diameters.
This guide covers design rules for laser-cut parts, based on numbers from Boda's published process data (along with any applicable standard). We’ll go over the materials available (aluminum, carbon steel, and stainless steel), typical tolerances, and the design choices that have an impact on price.
KEY TAKEAWAYS: KMC GREEN CHECKLIST CARDKey Takeaways
Laser cutting tolerance is ±0.45 mm linear (±0.20 mm on high precision) and ±0.12 mm on hole diameter (±0.08 mm on high precision).
Sheet metal parts need a hole diameter of at least 0.6×T (on 0.5 to 10 mm sheet) or 0.4×T (on 10 to 20 mm sheet).
Holes must be spaced at least 2×T from edges and 5×T from other holes.
To prevent them from deforming during bending, holes require a clearance from bends equal to at least 2×T + the bend radius.
When submitting your part for a quote, send your design as a STEP, STP, or SLDPRT file built using a sheet metal module, not as 2D files.
Table of Contents
How to Prepare a Design File for Laser Cutting
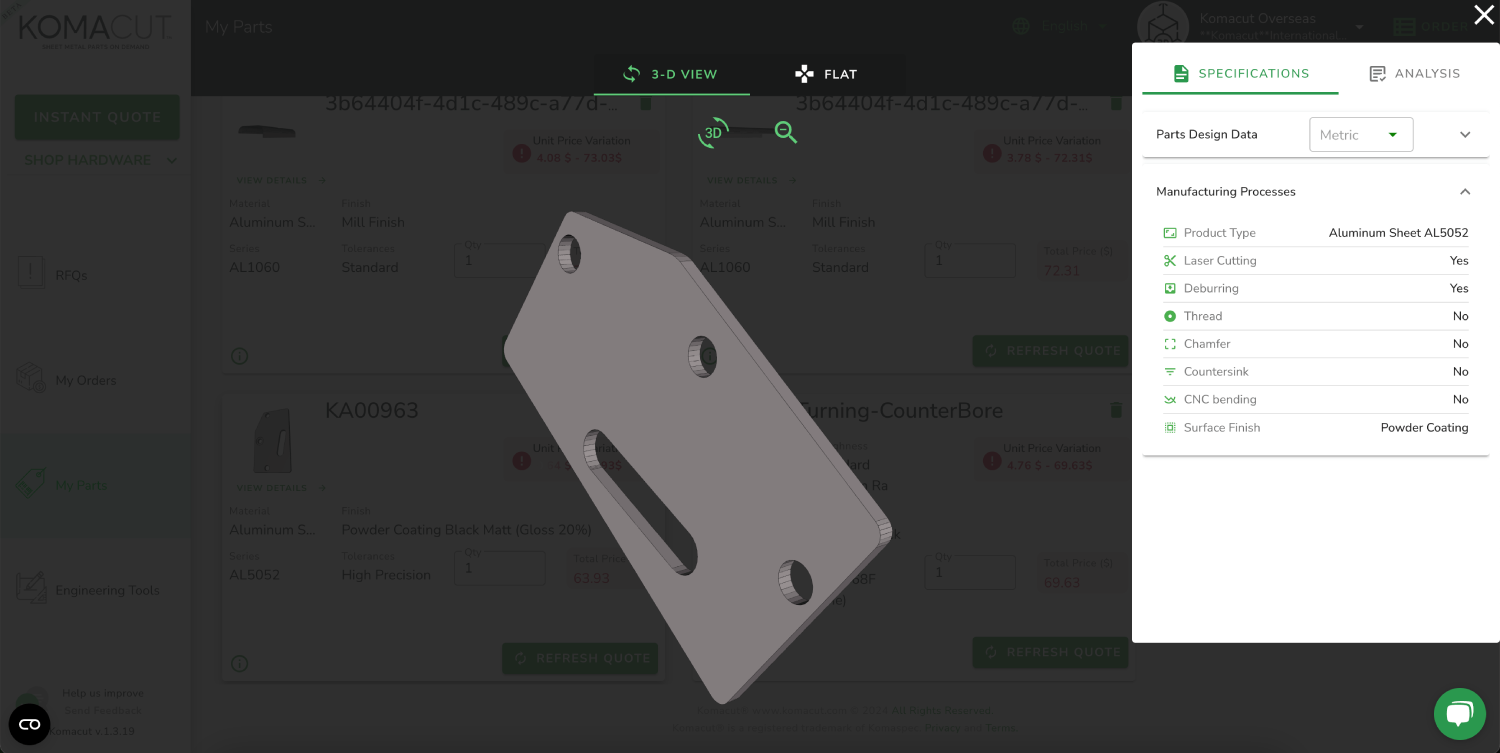
Send the manufacturer a 3D model of your part built as a sheet metal body. Boda's platform accepts STEP, STP, and SLDPRT files.
When uploading a design to Boda, the platform automatically reads the part’s thickness, bends, holes, threads, and countersinks straight from the geometry. Then, it provides you with DFM feedback and pricing.
CENTERED FIGURE (1200px max): dfm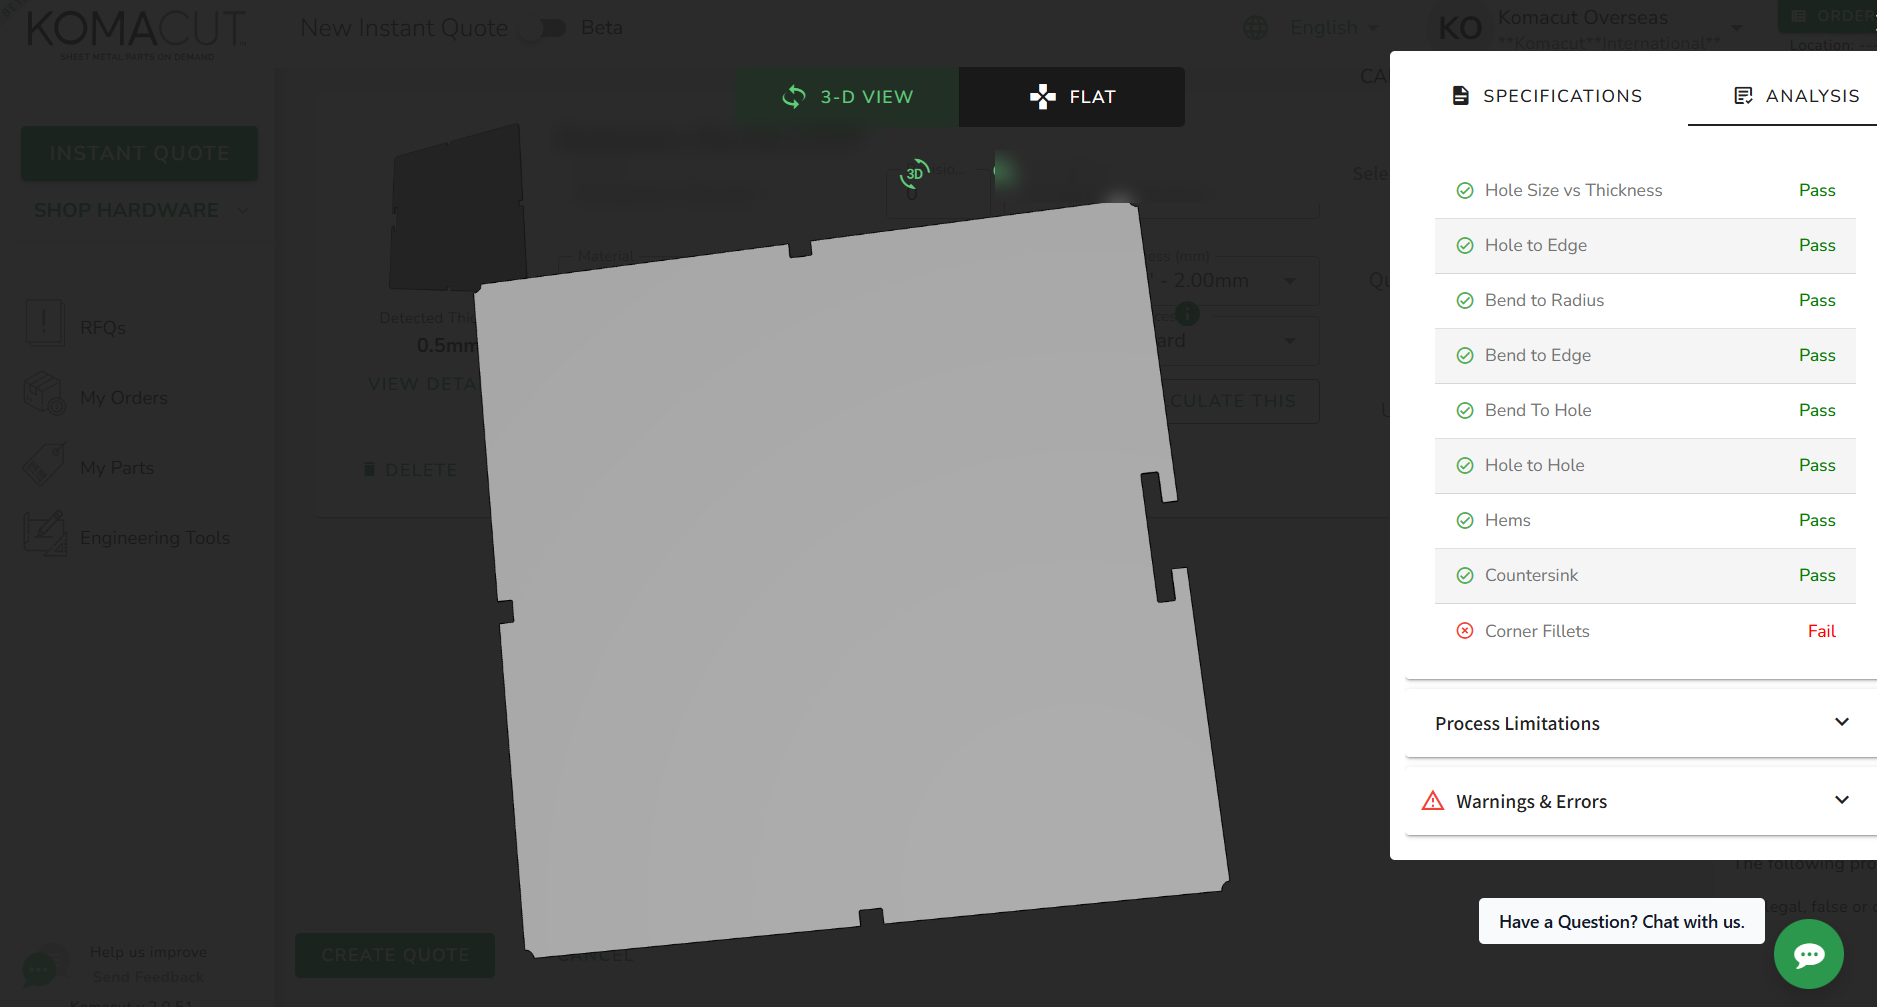
A 2D drawing doesn’t carry that geometry, and a part modeled as a plain extruded solid can't be unfolded reliably. Build the model with the sheet metal tools in your CAD software from the start.
Here are some best practices that will keep your design from getting flagged and requiring revisions:
- Model at a 1:1 scale using the material thickness you plan to actually use for your part. If you’re building a 3 mm part but you modeled it at 3.2 mm, your quote will be based on the 3.2 mm thickness.
- Model all countersinks and threaded holes as features. That way, the platform can detect them and include them as secondary operations in your quote.
- Keep every cut contour closed.
- Delete any duplicate or overlapping lines before exporting your design.
- Draw your part at nominal size. The manufacturer’s cutting program will offset the beam path by half thekerf width, so compensating for the beam in CAD will result in your part being cut undersized.
If the tolerance on any feature needs to be tighter than standard, include a PDF drawing that shows this. On its own, the 3D model represents your part’s geometry, while your drawing shows your intent.
Only do this for dimensions that affect fit or function, because specifying tighter tolerances adds inspection time and cost.
But what if you only have a sketch or 2D drawing of your part? In that case, use Boda's3D CAD drafting service. For a $15 flat fee, we will convert your drawing into a quotable 3D model within 5 business days.
CENTERED FIGURE (1200px max): fig2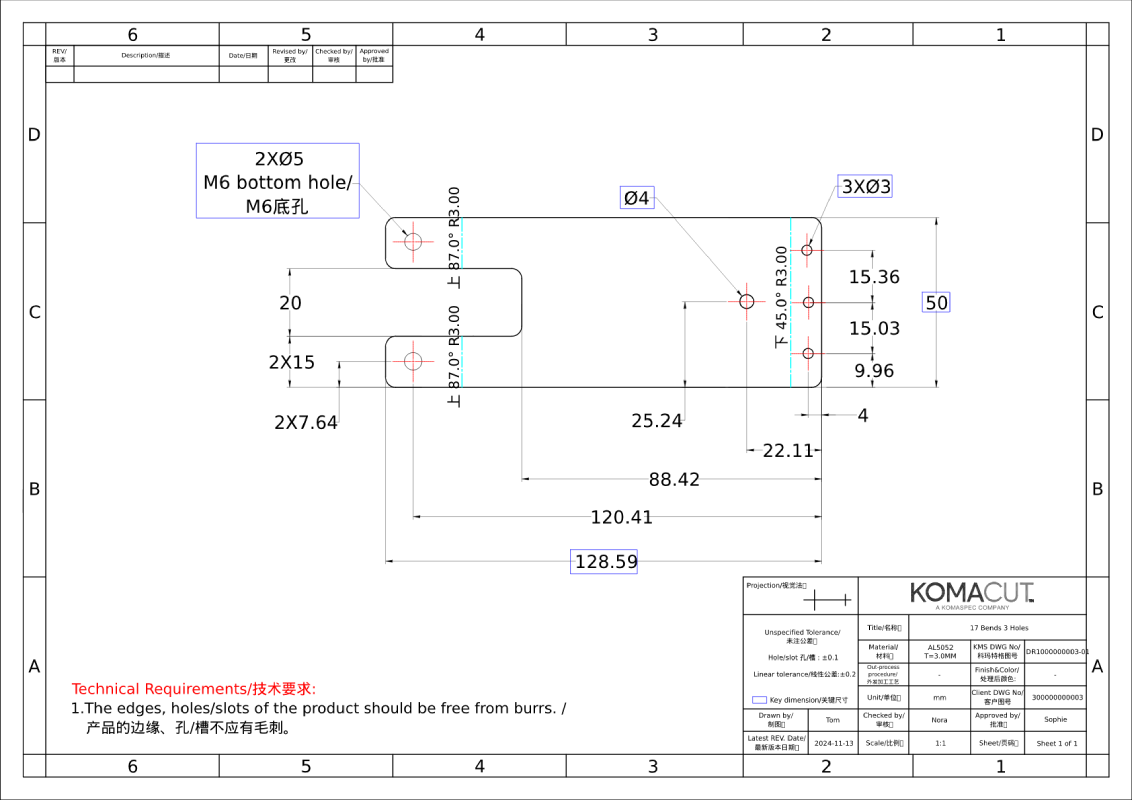
What Are the Design Rules for Laser Cut Parts?
It varies across manufacturers, but these are the design rules that apply on Boda's platform.
| Feature | Rule | Example at T = 3 mm |
|---|---|---|
| Minimum hole diameter (T 0.5–10 mm) | ≥ 0.6 × T | 1.8 mm |
| Minimum hole diameter (T 10–20 mm) | ≥ 0.4 × T | 4.8 mm at T = 12 mm |
| Hole to edge | ≥ 2 × T | 6 mm |
| Hole to hole | ≥ 5 × T | 15 mm |
| Inside corner radius | ≥ 0.5 × T | 1.5 mm |
| Countersink depth | ≤ 0.6 × T | 1.8 mm |
Table 1: Boda DFM rules for laser cut sheet metal. Source: Boda platform DFM rules, also listed in ourlaser cut steel guide.
CENTERED FIGURE (1200px max): svg1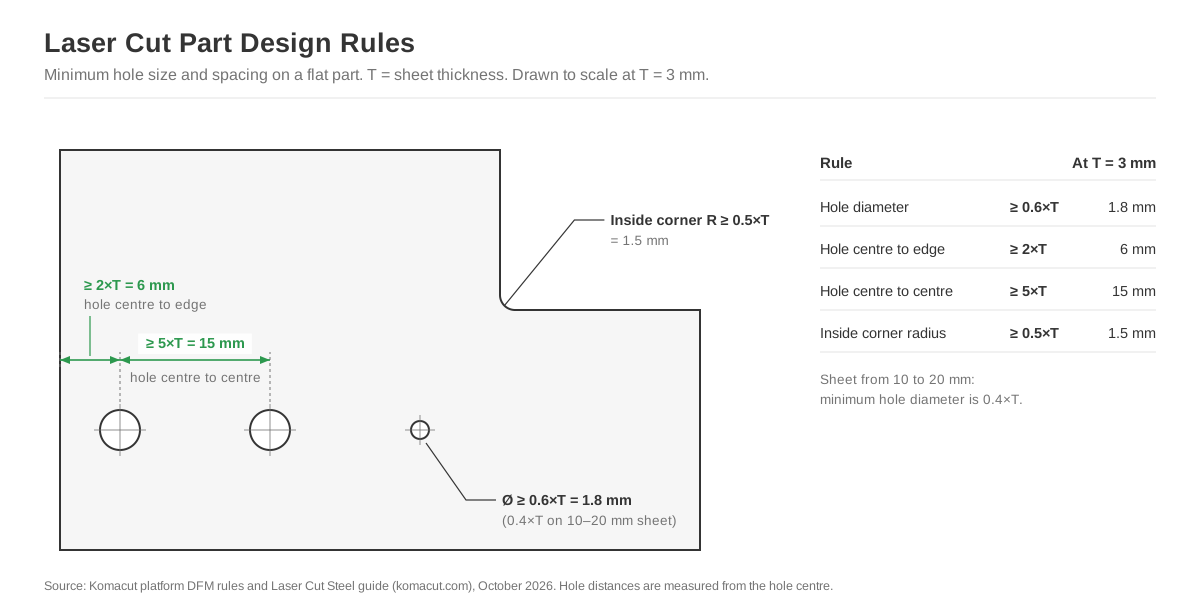
Every feature on this table scales with sheet thickness, so a rule that is generous for 1 mm sheet becomes tight when applied to 6 mm plate.
Minimum hole size depends on material thickness because the laser has to pierce through the sheet before it can trace a contour. And a very small hole on a thick plate leaves too little room for the laser to pierce through. This is why a 2 mm hole won’t work on a 6 mm sheet, but a 4 mm hole will.
It is possible to cut corners that fall below 0.5×T (for Boda, the real minimum is R0.2 mm). So instead of rejecting these corners outright, our platform simply flags them as sharp corners. But default to the stated 0.5×T minimum radius because it removes a stress riser and doesn’t cost anything to do in CAD.
As for the kerf,TRUMPFnotes that a focused beam is "often less than half a millimeter" across, creating a kerf that is "barely wider" than this. That allows the laser to cut fine slots, but it doesn't make thin webs strong. So apply the 2×T hole-to-edge rule to webs between cutouts. Treat any fine protrusions as fragile because they risk bending during deburring or handling.
Holes, Threads, and Countersinks
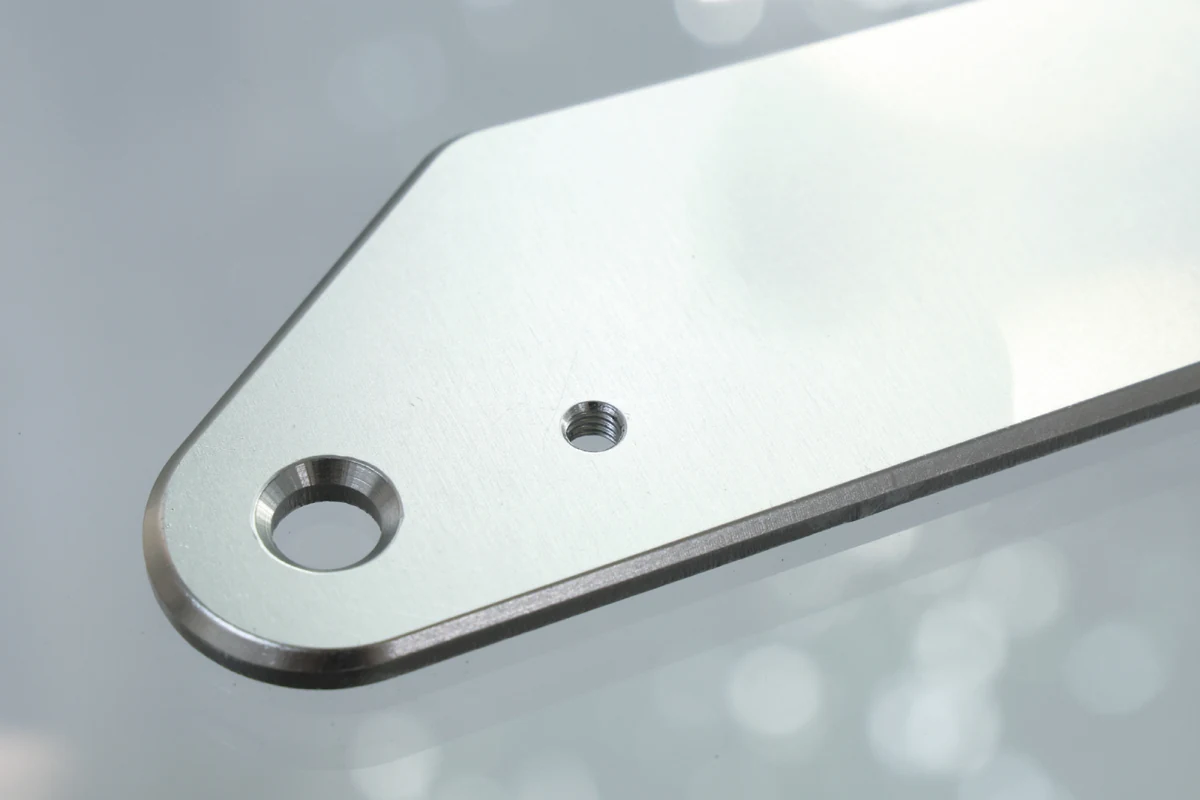
Holes can be made with laser cutting, but a laser can’t do the tapping, chamfering, and countersinking. Each of these is a secondary operation done after the hole has been cut.
IMAGE ROW: THREADS AND COUNTERSINKS - TEXT LEFT / IMAGE RIGHTIf a hole will be tapped, size it to the tap drill, not the screw. In the case of ISO metric coarse threads, the tap drill is sized at approximately the nominal diameter minus the pitch. To be more specific, theISO 724 thread tablelists 4.2 mm for M5 × 0.8, 5.0 mm for M6 × 1.0, and 8.5 mm for M10 × 1.5. If you model the thread in CAD, the platform will size the pilot hole for you.
Be aware that these secondary operations all have limits of their own. Tapping and countersinking require sheet that’s 1.6–20 mm thick, and the part must be no more than 400 × 400 mm unfolded. The depth of a countersink needs to be 0.6×T or less. Any deeper and the cone will eat through the sheet.
Rules for Laser Cut Parts That Will Be Bent
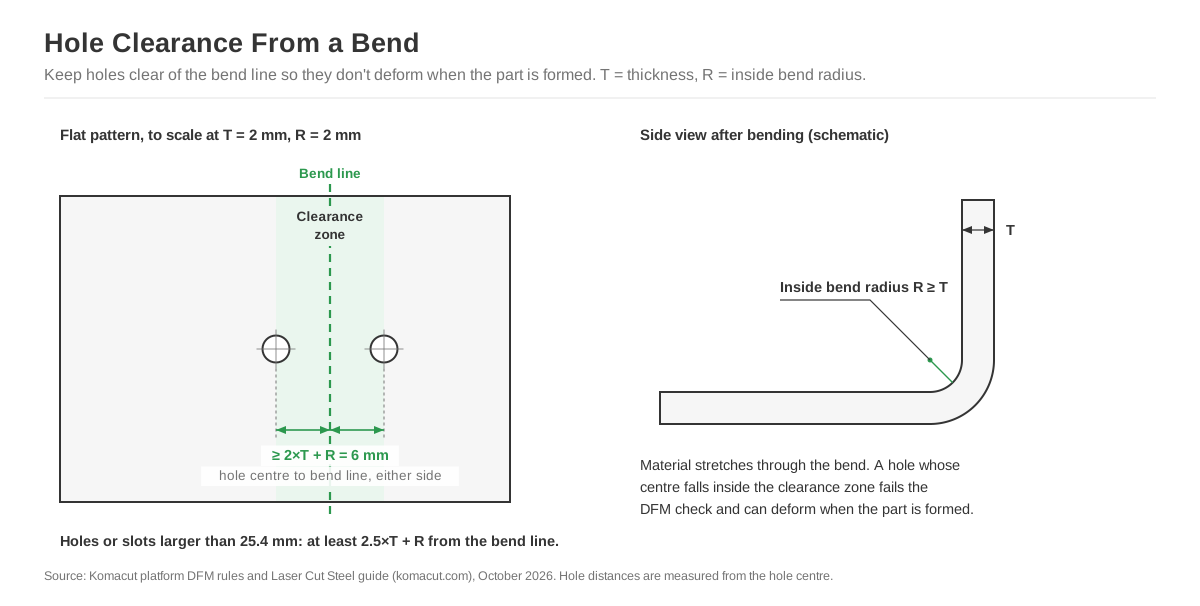
After being cut, most parts will be bent on a press brake. This causes the material to stretch at the bend, and any hole that’s been placed too close to the bend will stretch along with it.
IMAGE ROW: BENT PARTS - IMAGE LEFT / TEXT RIGHT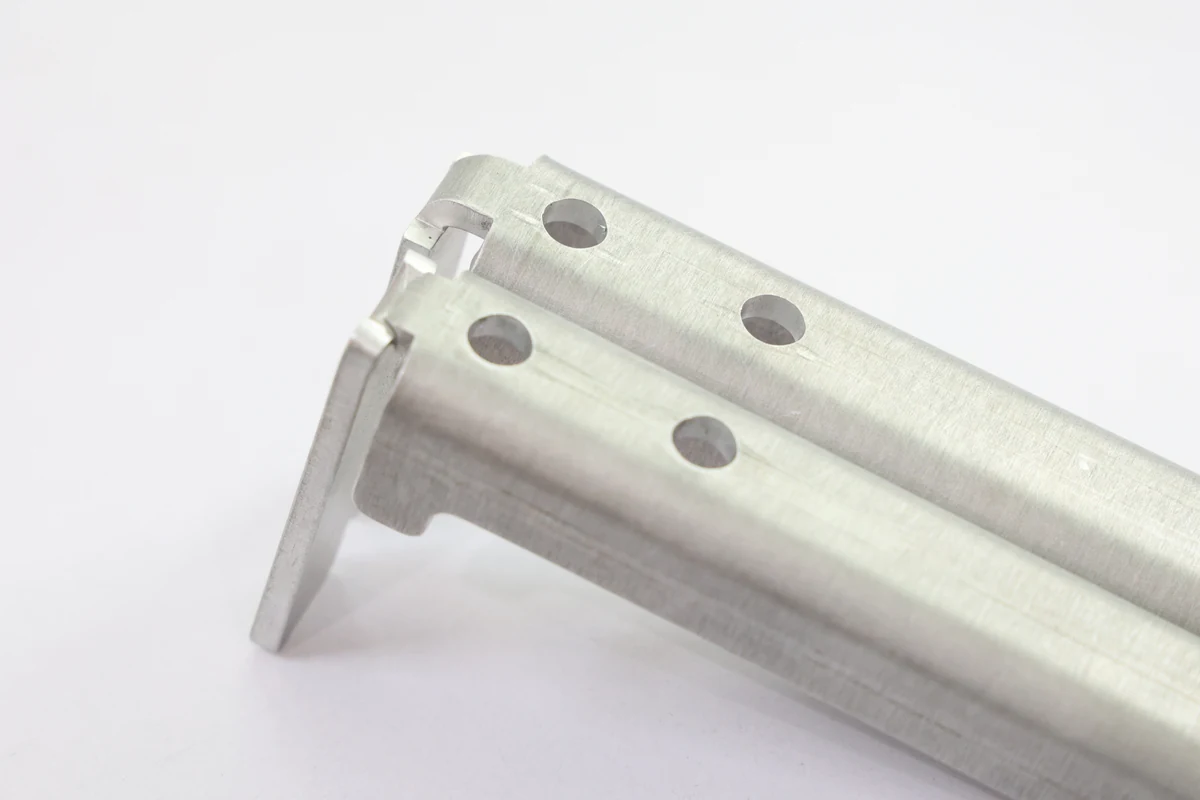
Use these rules to keep features clear of bends, where R is the inside bend radius:
| Feature | Rule |
|---|---|
| Hole (25.4 mm diameter or less) | ≥ 2×T + R from the bend |
| Hole or slot (above 25.4 mm) | ≥ 2.5×T + R from the bend |
| Bend to part edge | ≥ 2.5×T + R |
| Inside bend radius | ≥ T |
| Hems | Sheet up to 2 mm only; inside diameter ≤ 2×T; return length ≥ 4×T |
Table 2: Design rules for features near bends.
To prevent the material from tearing at the corner, add bend reliefs for any bend that meets another bend or ends at an edge.
Boda can bend parts up to 2,400 mm long and 10 mm thick. For radii and angle tolerances, consult our page onCNC sheet metal bending.
How Do You Choose the Right Material for a Laser Cut Part?
Start with a material that is suitable for your part’s intended application, then check whether the grade and thickness are stock items.
Boda'smaterials pagelists which materials are carried at each of our facilities:
| Family | China facility | Mexico facility |
|---|---|---|
| Carbon steel | SPCC, Q235, Q275, Q355, SAPH440, #20, 65Mn | A366, A715, A36, A572 |
| Galvanized steel | SGCC | — |
| Stainless steel | SS301, SS304, SS316, SS316L | SS304, SS316, SS316L |
| Aluminum | AL1060, AL5052-H32, AL6061-T6, AL6063-T5, AL7075-T6 | AL5052-H32, AL6061-T6 |
Table 3: Sheet metal grades by facility
IMAGE ROW: MATERIALS - TEXT LEFT / IMAGE RIGHTIf your design is for an indoor enclosure or bracket that will be powder coated, your best bet is likely cold-rolled SPCC. But for an outdoor application (or a part that will be around a lot of moisture), SS304 is likely a better choice (or aluminum if you need to limit the part’s weight). If you’re making an aluminum part that bends, go with AL5052-H32 (AL6061 is prone to cracking at the bend).
Standard gauges are stock items, so design your part based on a standard thickness. If your part requires an off-size sheet, the material will have to be sourced separately, which adds cost and lead time (even for a simple design). The thickness tolerance of the sheet itself is set by the mill standard (e.g.ASTM A568for carbon steel sheet), which is one more reason to leave clearance in slots that receive tabs.
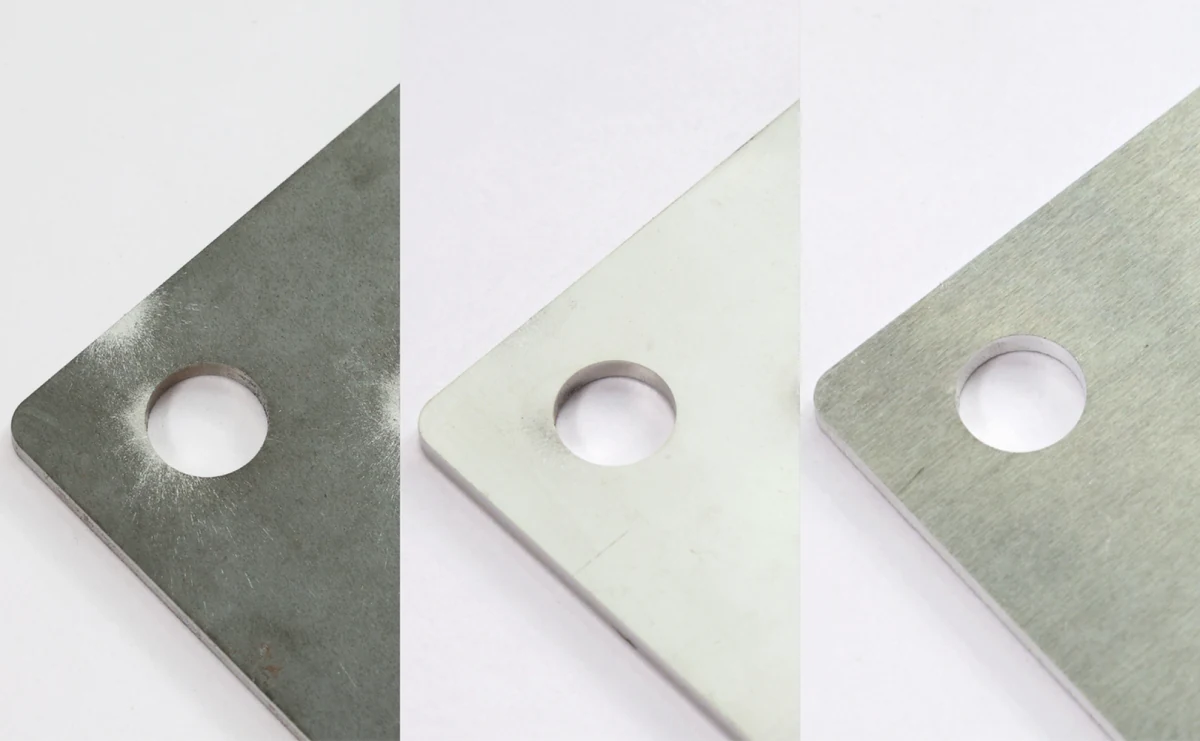
Laser cutting can accommodate sheets up to 20 mm thick, but your maximum part size will depend on the type of sheet you’re using:
| Q235 / Q355 | SAPH440 | SPCC | SGCC | Aluminum | Stainless steel |
|---|---|---|---|---|---|
| 1,500 × 3,000 mm | 1,260 × 2,500 mm | 1,250 × 2,500 mm | 1,250 × 2,500 mm | 1,220 × 2,440 mm | 1,220 × 2,440 mm |
Table 4: Maximum sheet size by material
What Tolerances Apply for Laser Cutting?
For Boda, standard laser cutting tolerance is ±0.45 mm on linear dimensions and ±0.12 mm on hole diameters. For high precision, linear tightens to ±0.20 mm and hole diameter goes down to ±0.08 mm.
| Tolerance | Linear | Hole diameter | Bend angle | Bend XYZ |
|---|---|---|---|---|
| Standard | ±0.45 mm | ±0.12 mm | ±1.0° | ±0.45 mm |
| High precision | ±0.20 mm | ±0.08 mm | ±0.5° | ±0.20 mm |
Table 5: Sheet metal tolerances. Source:Boda process tolerances.
Stick to standard tolerance unless there’s a good reason not to. You should only specify high precision for features that are designed to mate with something (e.g. slots for dowels, tab-and-slot joints, locating holes). Otherwise, you’re adding inspection time to your part without actually improving it.
When requesting a quote, you will also pick a generalISO 2768-1tolerance class (fine, medium, or coarse). The class you choose will be applied to every dimension you haven't specifically called out.
The right clearance will factor in how the tolerances of different features might pair up in an assembly. If your part has a 3 mm tab, cutting the slot at 3.2 mm gives it enough room for potential variations in sheet thickness and covers the cutting tolerances of both parts. That way, the tab will fit effortlessly, without needing to be filed down.
Make sure your required tolerances are all stated explicitly. Your vendor will simply go with their default unless the drawing specifies otherwise. And if you specify a ±0.05 mm requirement on a slot, this goes beyond what laser cutting can do. It will need to be done with secondary machining, which should get figured into your initial quote rather than being a surprise you discover at inspection.
For more details on tolerances, check out oursheet metal tolerances guide.
What Affects the Cost of a Laser Cut Part?
When you’re designing a part, you can influence the cost via your choice of material and the machine time needed to fabricate the part. These are the cost factors that are within your control.
The thickness of the material.To minimize costs, use the thinnest sheet that is capable of carrying the load. Choosing 2 mm sheet instead of 3 mm will cut down on the material weight and, asTRUMPFnotes, a thinner sheet also cuts faster. Use oursheet metal weight calculatorto compare the weight of your blank in different thicknesses.
The number of features.Every internal cutout on your design will require a separate pierce and a separate contour. A plate with 50 small ventilation holes will need 50 separate pierces to get them all done. Replace those with six slots and you’ll cut it down to only six pierces. Where it won’t compromise function, reduce feature count by combining holes into slots.
IMAGE ROW: COST - IMAGE LEFT / TEXT RIGHT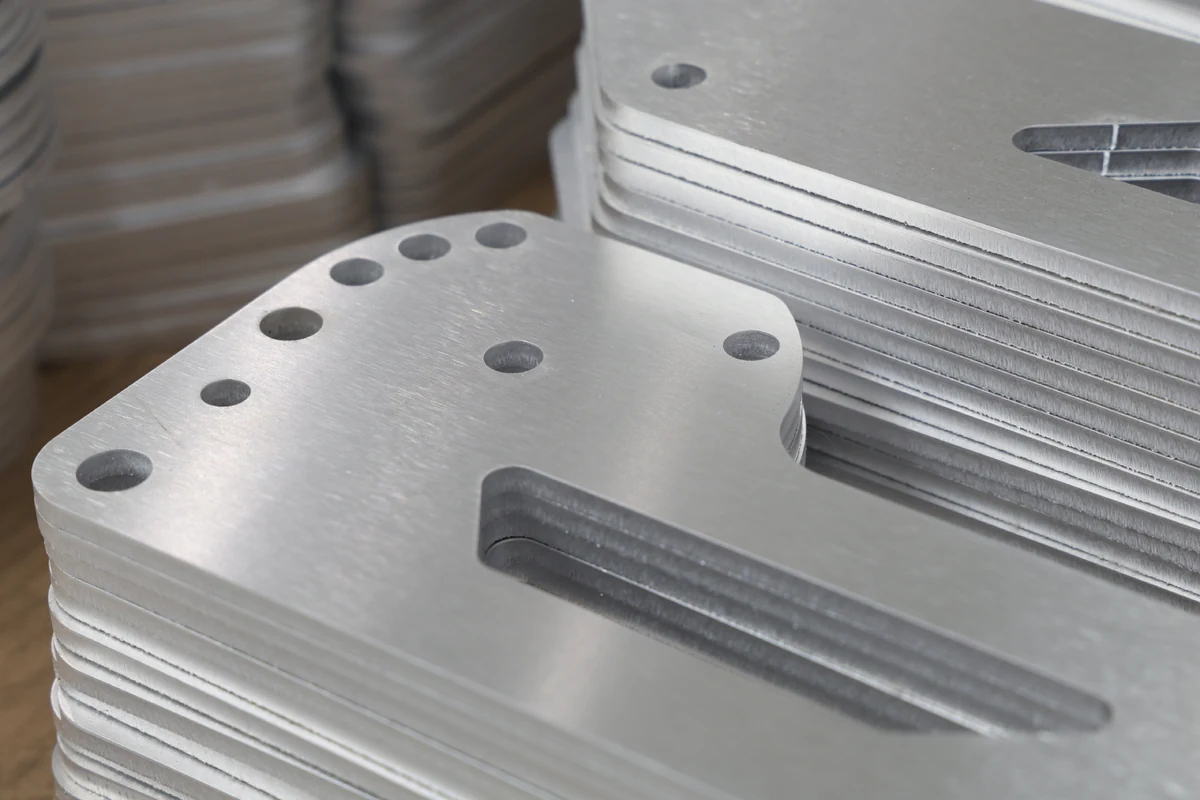
How well the part nests on the sheet.Parts that nest tightly on the sheet create less waste. Rectangular outlines and shared orientations nest better than odd shapes. Ournesting calculatorshows how many parts fit on a sheet and the material yield.
Any surface finish that is applied to the part.Powder coating, plating, and anodizing will add cost and lead time (and may reduce your maximum part size). Going with a pre-finished sheet (e.g. brushed stainless) means you can avoid the added finishing step (but in this case, the laser cut edges will be bare metal, so make sure to finish the part after cutting if the edges need protection). See oursurface finishing pagefor a comparison of the different options.
The number of sharp corners.Keeping your inside corner radii at 0.5×T or more adds no extra cost and removes sharp points that would need deburring.
Consult ourlaser cutting price guidefor a more precise breakdown.
DFM Checklist
Before uploading your design, run it through the following checklist:
- Design is in STEP, STP, or SLDPRT and built as a single sheet metal body
- Modeled at 1:1 scale with a standard stock thickness
- Holes ≥ 0.6×T (≥ 0.4×T for sheet thicker than 10 mm)
- Holes ≥ 2×T from edges and ≥ 5×T from other holes
- Inside corner radii kept at ≥ 0.5×T
- Holes ≥ 2×T + R from bends; bend reliefs added
- Threads and countersinks are modeled as features
- The part falls within the material’s max sheet size
- PDF drawing attached for any tolerance tighter than standard
Boda CTA: SOFT-WASH FULL FRAME (BEFORE FAQ)
Instant DFM Checking
Check Your Design Before You Order
Upload your STEP file to the Boda platform and get a price with DFM feedback against all our design rules in about 30 seconds. For parts ready to order, seelaser cutting services.
Frequently Asked Questions
What is the minimum hole size for laser cutting?
It depends on the vendor. For Boda, the minimum diameter is 0.6 times the sheet thickness (or 0.4 times the thickness for sheets 10 mm or thicker). So hole diameter must be at least 1.8 mm when cut on 3 mm sheet. Going below the minimum would give the laser too little room to pierce cleanly, which could distort the holes.
What tolerance can laser cutting hold?
For Boda, the standard tolerance is ±0.45 mm linear (±0.20 mm on high precision) and ±0.12 mm for hole diameters (±0.08 mm on high precision). Any tolerances tighter than this (e.g. ±0.05 mm for a slot) will require secondary machining and should be called out on the drawing to ensure an accurate quote.
What file format do I need for laser cut parts?
Boda accepts 3D models in STEP, STP, or SLDPRT format, so long as they’re built with a sheet metal module. If you only have a 2D drawing for your part, you can use a CAD drafting service to convert it into a 3D model that can be submitted for quoting.
How close can a hole be to a bend?
If the hole is 25.4 mm in diameter or less, it should have a minimum distance of two times the material thickness plus the inside bend radius from the bend line. For larger holes and slots, leave at least 2.5 times thickness plus the radius. Place the hole any closer and it will deform when the material is bent.
Do laser cut parts need corner radii?
Your part’s inside corners should have a radius of at least 50% of the material thickness. Boda is capable of cutting inside corners down to R0.2 mm, but our automated DFM check will flag any radius under 0.5×T as a sharp corner. Adding a corner radius costs nothing, removes a stress concentration and reduces deburring on the finished part.