
- Key Takeaways
- Which Metal Surface Finish Should You Choose?
- Surface Finishing Process vs. Surface Finish
- Surface Finishes for Sheet Metal Parts
- 1. Powder Coating
- 2. E-Coating
- 3. Zinc Plating
- 4. Galvanizing
- 5. Anodizing
- 6. Passivation
- 7. Brushed Finish
- 8. Mill Finish
- 9. Antirust Oiling
- Sheet Metal Finishes Comparison Chart
- How Do You Design Sheet Metal Parts for Finishing?
- How to Specify a Finish on a Drawing or in a Quote
- Frequently Asked Questions
Metal surface finishing refers to the treatments or coatings applied to the surface of a metal part after that part has been cut, shaped, and the hardware has been installed. These finishes are applied to give the metal additional corrosion resistance, resistance to wear, certain electrical properties, or a specific appearance. For sheet metal parts, nine finishes cover almost every real order: powder coating, e-coating, zinc plating, galvanizing, anodizing, passivation, brushed, mill finish, and antirust oiling.
Choosing the right finish comes down to three factors: 1) the base material, 2) the corrosion risk, and 3) how thick the coating can be before it causes problems for your part's tolerances and hole sizes.
In this article, we'll help you answer each of those questions so you can specify the right finish on your drawing and avoid problems that would surface in incoming inspection.
KEY TAKEAWAYS: KMC GREEN CHECKLIST CARDKey Takeaways
Sheet metal finishes add a layer to a part's surface or alter the metal's properties at that surface, usually to provide additional protection or alter its appearance.
Powder coating is the default cosmetic finish for sheet metal parts, and accounts for more than 15% of the whole industrial finishing market.
Certain finishes add thickness to the surface of a part, which can push holes and fits outside their tolerances.
Mill finish is not a finishing process but instead refers to the properties of the material's surface when it leaves the mill.
Table of Contents
- Key Takeaways
- Which Metal Surface Finish Should You Choose?
- Surface Finishing Process vs. Surface Finish
- Surface Finishes for Sheet Metal Parts
- Sheet Metal Finishes Comparison Chart
- How Do You Design Sheet Metal Parts for Finishing?
- How to Specify a Finish on a Drawing or in a Quote
- Frequently Asked Questions
Which Metal Surface Finish Should You Choose?
Choose the finish based on the material it will be applied to and the part's intended environment (e.g., indoor vs. outdoor, high vs. low corrosion exposure).
| Material | Service condition | Recommended finish | Why |
|---|---|---|---|
| Carbon steel (SPCC, Q235, SAPH440) | Hidden internal part, will be machined or welded later | Antirust oiling | 24h salt spray protection for transit and storage; nothing to strip before the next operation |
| Carbon steel | Indoor, low visual, needs electrical grounding | Zinc plating (trivalent) | Conductive, 5-25 µm so holes stay in tolerance, 48-96h salt spray protection |
| Carbon steel | Indoor, visible | Powder coating | Color and texture; hard cured film |
| Carbon steel | Outdoor or humid | Powder coating (or e-coat + powder for coastal and industrial sites) | 480-1,000h salt spray protection; e-coat primer covers recesses missed by powder |
| Carbon steel | Complex geometry with internal channels, low visual | E-coating | Electrodeposition reaches surfaces spray cannot |
| Carbon steel | Outdoor structural, appearance irrelevant | Galvanizing (or pre-galvanized SGCC sheet, with pretreatment and powder coat if color is needed) | Thick sacrificial zinc layer; low cost per part |
| Stainless steel (SS304, SS316) | Visible indoor panel | Brushed | Uniform grain hides handling marks; no coating to chip |
| Stainless steel | Food, medical, marine, wet environments | Passivation | Removes free iron picked up in cutting and forming so the chromium oxide layer can form fully |
| Aluminum (AL5052, AL6061, AL6063) | Visible, wear surface, or needs electrical insulation | Anodizing (natural or black) | Oxide layer is part of the metal so it cannot peel |
| Aluminum | Must match a RAL or Pantone color | Powder coating | Only finish on aluminum with a color range |
| Any material | Prototype or internal part, no exposure | Mill finish | Lowest cost, no size limit, no added thickness |
For outdoor parts, write the intended environment on the drawing using theISO 12944-2corrosivity categories, which range from C1 (for heated interiors) to C5 (for high-salinity coastal and humid industrial sites).
Surface Finishing Process vs. Surface Finish
The finishing process refers to the method used to achieve the desired surface (for example, powder coating). The surface finish is the result of that process (for example, 100 µm thick 90-gloss black polyester film).
Make sure to specify the finish on your drawing, because the same process could yield different results depending on how it's performed. Some surfaces are also only achievable using two processes, so specifying the outcome you want is the best way to ensure you get the right result.
Surface roughness (Ra) is a separate topic, which has to do with machined texture rather than finishing. It is covered in ourguide to CNC machining surface roughness.
Surface Finishes for Sheet Metal Parts
The thickness figures, neutral salt spray (NSS) hours, material compatibility, and maximum part size for each type of finish in this list are the ones used on the Boda platform.
The NSS tests are run to theASTM B117standard. But as the standard itself points out, cabinet hours do not necessarily correlate with how long the protection will actually last in the field. Use these numbers to compare options rather than to predict any exact duration.
1. Powder Coating
Powders used for coating contain resin, curing agents, and pigments. The powder is applied by spraying it on the surface of a grounded part using an electrostatic gun. It is then melted and cross-linked in an oven.
This is the default cosmetic option for enclosures and brackets. And according to thePowder Coating Institute, powder coating accounts for more than 15% of the industrial finishing market.
| Thickness | 70-150 µm |
|---|---|
| Salt Spray | 480-1,000h NSS (depending on pretreatment and powder class) |
| Materials | Aluminum, carbon steel, stainless steel |
| Max Part Size | 2,400 × 1,800 × 1,200 mm (this is larger than our bending envelope, so anything Boda can bend, it can powder coat as well) |
| Visual Grade | High (Boda stocks 13 colors by RAL or Pantone number, along with 3 blacks at 20% gloss, 90% gloss, and a Sandtex texture) |
| Cost | Mid (high with an e-coat primer) |
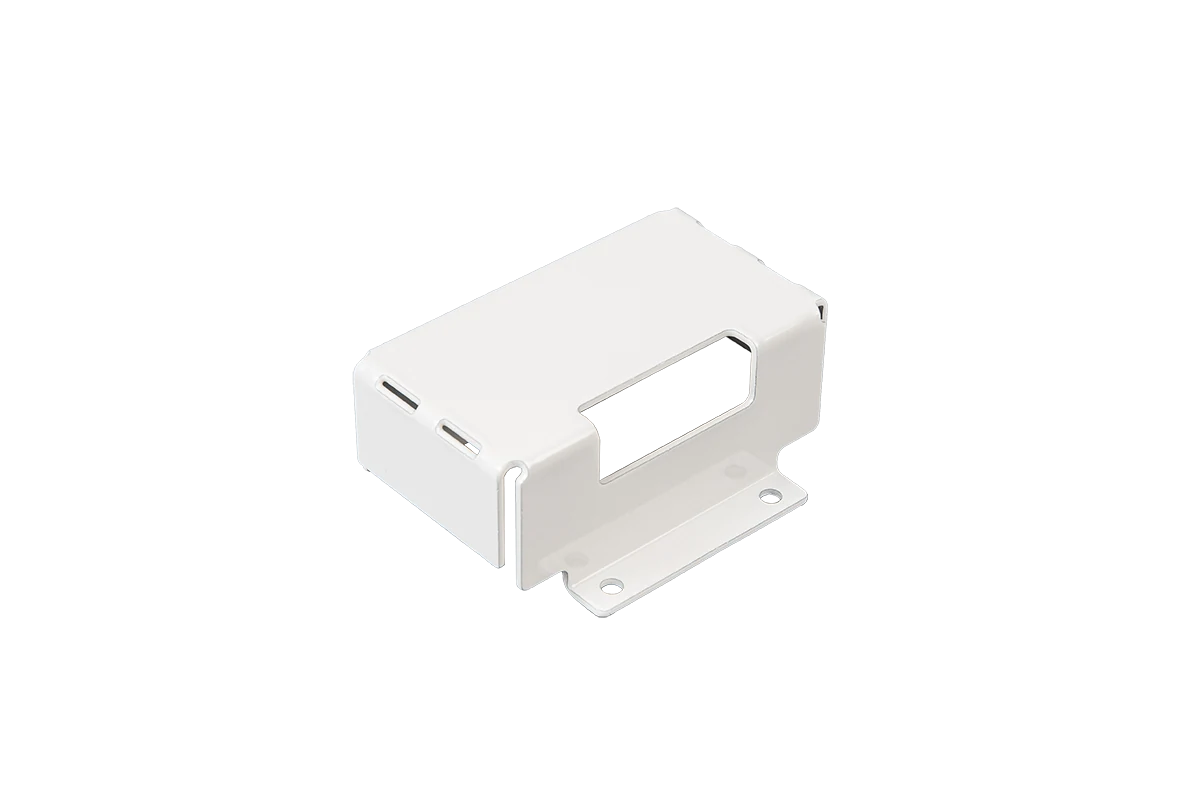
Opt for powder coating if the surface will be visible, needs to be colored, or if the part will be housed outdoors.
Avoid powder coating if the surface has to be conductive, has any holes with tight tolerances (±0.1 mm after coating), or when a thread cannot be masked.
Pretreatment decides whether a powder-coated part survives 480 or 1,000 hours of salt spray. Boda'sguide to avoiding powder coating quality issuescovers what happens before the gun.
2. E-Coating (Electrophoretic Coating)
This process involves submerging the part in a bath of water-based paint and using a DC electrical current to deposit paint on all of its wetted surfaces. The thickness of the resulting film depends on the current used.
According to theElectrocoat Association, e-coating gives complex parts 100% coverage with a uniform film thickness throughout (including recesses and edges).
| Thickness | 5-25 µm |
|---|---|
| Salt Spray | 96h NSS (or better) |
| Materials | Carbon steel, stainless steel |
| Max Part Size | 1,500 × 600 × 300 mm |
| Color | Black only |
| Visual Grade | Low |
| Cost | Low |
E-coating is well-suited for parts that are box- or tube-shaped and whose interior surfaces matter (since powder coating would either miss those surfaces or leave too thin of a layer) or parts with sensitive tolerances (at up to 25 µm of thickness, e-coating changes hole diameter by only 0.01-0.05 mm).
UV exposure will cause the epoxy to chalk. Outdoor parts need powder coating on top. That combination gives steel stronger corrosion resistance than either finish on its own.
3. Zinc Plating
Zinc plating can only be applied to carbon steel. It involves putting the part through an electrolyte bath and electrodepositing zinc onto its surface.
The plating is a protective barrier, with a corrosion rate 10 to 100 times slower than steel, according to theAmerican Galvanizers Association. And because zinc acts as an anode to steel, a part will continue to resist rust at a scratch even though the barrier has been compromised there.
| Thickness | 5-25 µm (the same 0.2-1.0 mil range the AGA lists for electroplated zinc underASTM B633) |
|---|---|
| Salt Spray | 48-96h NSS |
| Materials | Carbon steel only |
| Max Part Size | 1,200 × 400 × 400 mm |
| Passivate | Trivalent blue-bright (the usual RoHS-compliant choice since B633 added non-hexavalent types) |
| Visual Grade | Low |
| Cost | Low |
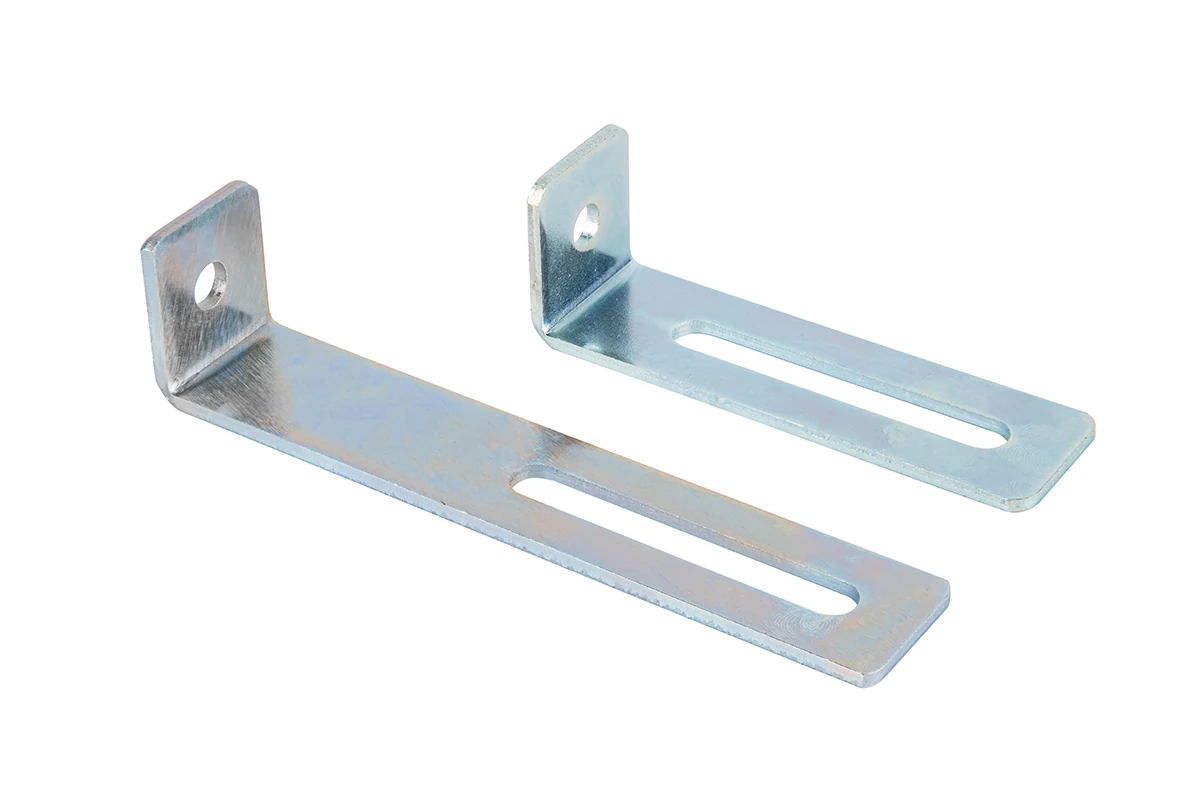
Use this finish for steel brackets on indoor products, parts that make up a chassis, and any part that will carry a current or take a ground strap.
The AGA rates electroplated zinc for interior exposure, which matches its 48-96h NSS rating.
Weld and thread before plating.
If powder coating over zinc, be aware that zinc doesn't work well as an undercoat. Make sure the part is pretreated for powder over zinc before coating.
4. Galvanizing
Galvanizing is another method that uses zinc to protect steel surfaces, and a few different processes fall under this umbrella.
Batch hot-dip galvanizing involves immersing a finished part in molten zinc. This gives the part a metallurgically bonded coating with a thickness that usually ranges from 50 to 200 µm.
Continuous sheet galvanizing (SGCC, ASTM A653) is where the raw sheet is coated at the mill.
Another option is using zinc-rich paint (sold as cold galvanizing), but this relies on a mechanical bond that has a fraction of the strength of a hot-dip coating.
| Thickness | Applied at the mill on SGCC sheet; hot-dip coatings run 50-200 µm |
|---|---|
| Salt Spray | Not published |
| Materials | Carbon steel (pre-galvanized SGCC, JIS G3302) |
| Max Part Size | Limited by SGCC sheet size, 1,250 × 2,500 mm |
| Visual Grade | Low |
| Cost | Material cost; no separate finishing step |
Unlike the other finishes here, galvanizing is supplied as pre-coated sheet rather than applied after fabrication. The hot-dip thickness above is an American Galvanizers Association figure, not a Boda platform value.
IMAGE ROW: GALVANIZING - TEXT LEFT / IMAGE RIGHTPre-galvanized SGCC sheet (yield ≥200 MPa, JIS G3302) is one of the standard carbon steel options for sheet metal parts, and it takes a powder-coated top finish with the right pretreatment. Because the zinc is applied at the mill before cutting, laser-cut edges on these sheets are bare steel. The zinc on the faces protects those edges sacrificially, but it doesn't wrap over the cut the way a post-fabrication hot-dip coating would.
Galvanizing is a good option for agricultural, utility, and outdoor structural parts where the appearance doesn't matter. But choose a different method for any surface that will be kept visible, parts with a tight fit, or anything that will be welded after the finish is applied.
5. Anodizing
Anodizing doesn't apply a coating to the part. Instead, it passes a current through an aluminum part while it's in an acid electrolyte bath to convert its surface into aluminum oxide. This oxide is hard, wear-resistant, electrically insulating, and porous enough so that it can be dyed before sealing.
So rather than a coating, as theAluminum Anodizers Councilpoints out, it's a layer that grows from the metal itself. Because the finish is part of the material, it can't peel or chip away.
| Thickness | 0.5-15 µm (the AAC puts interior commercial anodizing at roughly 2.5-5 µm and architectural Class II at 10-18 µm, while MIL-A-8625 Type III hardcoat, which is 50 µm and up, is a different process) |
|---|---|
| Materials | Aluminum only (AL1060, AL5052 H32, AL6061 T6, AL6063 T5, AL7075 T6) |
| Max Part Size | 1,500 × 1,000 × 400 mm |
| Colors | Natural and black |
| Visual Grade | High |
| Cost | Low to Mid |
Anodizing is a good choice for visible aluminum, surfaces that rub against other surfaces, and enclosures or heat sinks that need an insulating surface.
The results you get will be based on the alloy you use. Per the AAC, the chromium in 5052 and 6061 gives thicker coatings a yellowish hue. So two different alloys anodized using the same exact process may not have a matching finish. For consistent color across alloys, specify black.
6. Passivation
Passivation is a chemical treatment for stainless steel. FollowingASTM A967, it involves immersing a stainless steel part in either nitric or citric acid. This removes free iron (left by tool marks, iron dust, iron deposits in welds, etc.), which would otherwise be a rust-initiation site. It also helps a passive chromium oxide film form on the metal's surface.
| Thickness | None (transparent film with no measurable thickness) |
|---|---|
| Materials | Stainless steel only (301, 304, 316, 316L) |
| Max Part Size | 900 × 800 × 400 mm |
| Visual Grade | Medium |
| Cost | Low |
If a stainless steel part has been laser-cut or formed on a press brake and will be used in a wet environment, passivate it. Same with any part that must be rated for food contact, used in pharmaceutical applications, or that will come into contact with the body.
While stainless steel has inherent corrosion resistance, a fabricated part may still rust where free iron is left on the surface. A967 includes a number of acceptance tests (salt spray, water immersion, copper sulfate, high humidity) to confirm the passivation has actually worked.
7. Brushed Finish
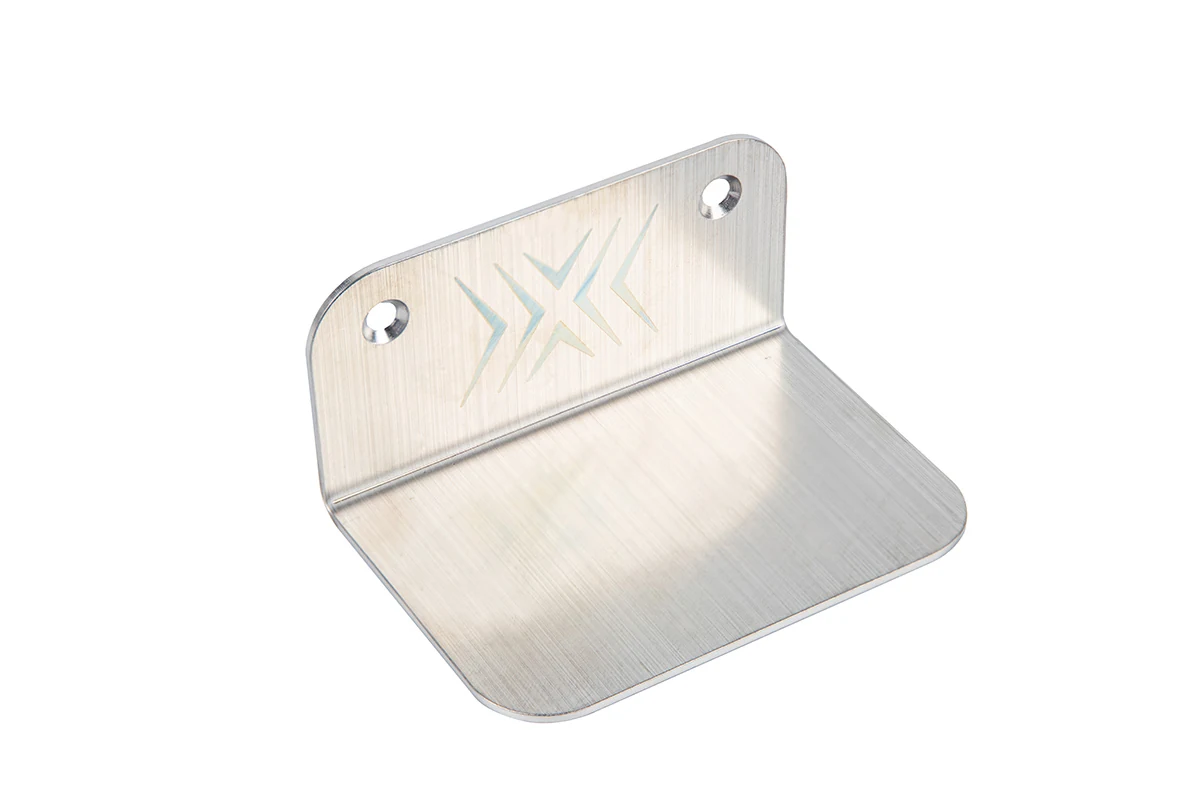
A brushed finish is the typical finish for visible stainless steel or aluminum panels. It is created by using an abrasive belt or brush to draw a uniform directional grain across the metal's surface. This removes a slight amount of material from the surface but does not add any protection. Instead, the results are cosmetic, hiding scratches and marks from handling and leaving the surface with a consistent satin look.
| Thickness | None |
|---|---|
| Materials | Stainless steel, aluminum |
| Max Part Size | 1,500 × 300 × 200 mm (the smallest envelope on this list) |
| Visual Grade | Medium |
| Cost | Varies (scales with area) |
For brushed parts, specify the grain direction against a datum edge. A manufacturer will only be able to brush the faces the belt can reach, so be clear about whether the grain must continue across bends.
On stainless steel, the brushed surface has an appearance close to the No. 4 finish in ASTM A480. But don't rely solely on this. Make sure to call out the desired look against an approved sample and not just the standard.
8. Mill Finish
Mill finish is simply the surface of the metal as it was after leaving the rolling mill (plus laser cutting and bending if it has been formed). It's a clean, slightly matte surface, which might have a faint rolling texture and maybe a light oxide line on any edge that's been cut. It doesn't provide any additional protection.
| Thickness | None |
|---|---|
| Materials | Stainless steel, aluminum (carbon steel is not offered as mill finish; it ships oiled instead) |
| Max Part Size | No maximum |
| Visual Grade | Low |
| Cost | Baseline |
Because it essentially leaves the surface as is, mill finish is generally reserved for prototypes, parts that are housed inside a coated enclosure, and aluminum or stainless steel parts that you will be finishing on your end. It should not be used for any surface that is visible to the customer.
9. Antirust Oiling
This is a thin layer of oil that gets applied to carbon steel before it is packed. It is intended to provide temporary rust protection while the material is being shipped or stored, before it will be machined or welded. It is not a service finish. Don't rely on it for the finished product.
| Thickness | None |
|---|---|
| Salt Spray | 24h NSS |
| Materials | Carbon steel only |
| Max Part Size | No maximum |
| Visual Grade | Low |
| Cost | Baseline |
The oil needs to be removed before the part can be coated. Oil left on the surface stops powder adhering in spots and gives an inconsistent application.
Sheet Metal Finishes Comparison Chart
| Finish | Thickness | Salt spray (NSS) | Materials | Max part size (mm) | Visual grade | Relative cost |
|---|---|---|---|---|---|---|
| Powder coating | 70-150 µm | 480-1,000h | CS, SS, Al | 2,400 × 1,800 × 1,200 | High | $$ |
| E-coating | 5-25 µm | ≥96h | CS, SS | 1,500 × 600 × 300 | Low | $ |
| Zinc plating | 5-25 µm | 48-96h | CS | 1,200 × 400 × 400 | Low | $ |
| Galvanizing | 50-200 µm (hot-dip); mill-applied on SGCC sheet | Not published | CS | Depends on process | Low | $$ |
| Anodizing | 0.5-15 µm | Not published | Al | 1,500 × 1,000 × 400 | High | $ |
| Passivation | None | Per ASTM A967 | SS | 900 × 800 × 400 | Medium | $ |
| Brushed | None | None | SS, Al | 1,500 × 300 × 200 | Medium | Quote |
| Mill finish | None | None | SS, Al | No limit | Low | Baseline |
| Antirust oiling | None | 24h | CS | No limit | Low | Baseline |
Figures for thickness, NSS, and max size are drawn from Boda's platform engineering tables; cost comparisons are based on numbers from Boda.
How Do You Design Sheet Metal Parts for Finishing?
Include the thickness of the coating when calculating tolerances.Powder coating a surface with holes will cause the diameter of those holes to close by 0.14 to 0.30 mm (exceeding the ±0.12 mm tolerance for standard laser-cut holes). The solution here is to add 0.3 mm to the hole size, mask the holes, or specify that the part should be dimensioned after coating. With zinc, e-coat, and anodize, this is rarely an issue since they only add minimal thickness (0.5-25 µm) and won't usually cause any clearance problems.
SVG CHART: METAL SURFACE FINISH COATING THICKNESS VS HOLE TOLERANCE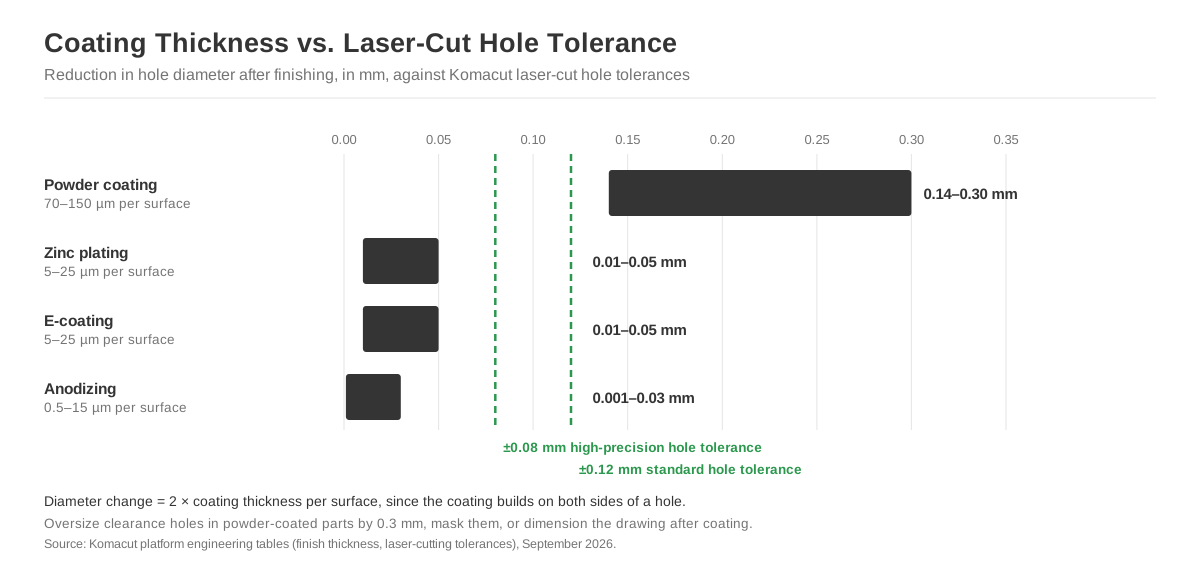
Mask any surface that has to remain bare, but expect a hang mark.Applying powder in an M4 thread means chasing every hole, so grounding pads, tapped holes, and mating faces should be marked as masked areas. Parts hang from a hook when they're dipped or sprayed, meaning there will be a bare area where the part was held (MIL-A-8625 has contact marks as part of its acceptance criteria for this reason). Add a small hole or tab in an area that won't be visible to the end user and designate it as the part's hang point.
Design for line of sight, and apply the finish last.Charged powder will be drawn to the nearest grounded edge. That means the mouth of a deep channel will collect powder while barely any adheres to its floor. Likewise, narrow U-channels and boxes with small openings will get coated unevenly. When the surface finish of the interior matters, go with e-coating. Thread and weld before coating. If this can't be done and something needs to be welded into the coated assembly, let the shop know so they can mask the weld zones.
SVG CHART: POWDER COATING VS E COATING DEEP CHANNEL COVERAGE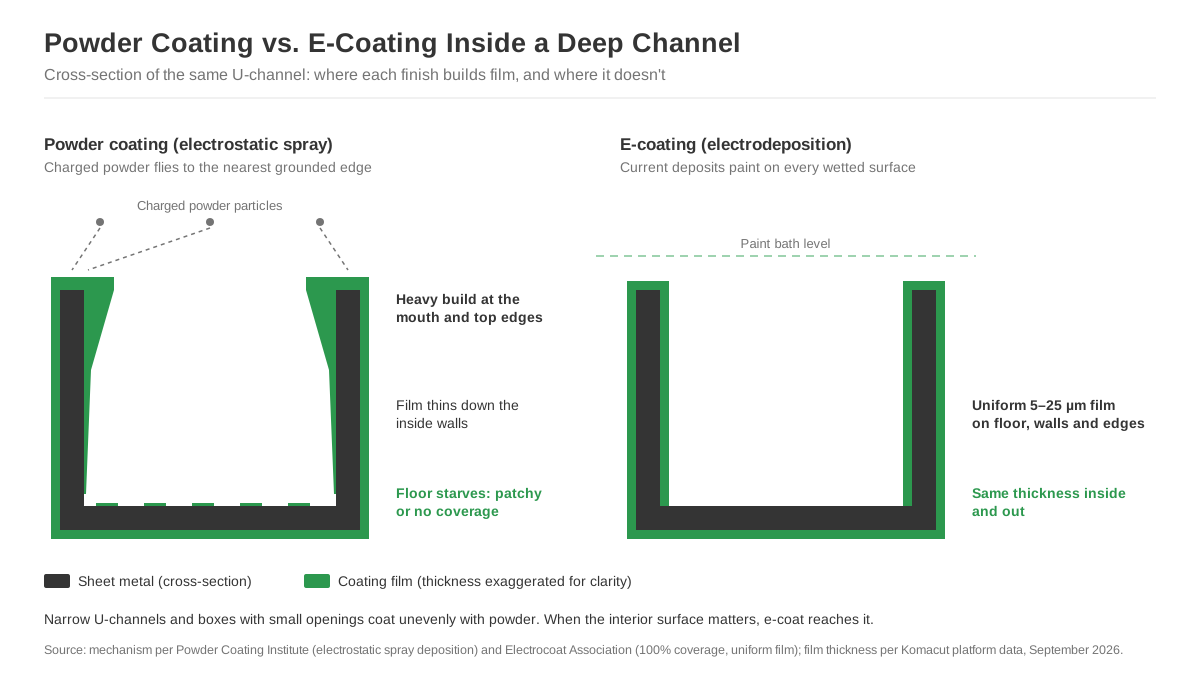
How to Specify a Finish on a Drawing or in a Quote
Name the finish and its color code (e.g., "Powder coat, RAL 9003 White, 20% gloss"), along with testable performance requirements (e.g., "≥480h NSS per ASTM B117" or "passivate per ASTM A967"). Then list which features will be masked, note the grain direction, and identify the hang point (where relevant). Finally, note whether the dimensions are for the coated part or the part before the surface finish is applied.
If you're using the Boda platform, you'll be able to choose the finish as part of your instant quote. You will only be able to choose finishes that are compatible with the material and part size you've selected, and your price will update with every change you make. For a full rundown on compatibility, consult oursurface finishing optionsandmetal materialspages. For envelopes, refer to ourprocess tolerancespage.
Boda CTA: SOFT-WASH FULL FRAME (BEFORE FAQ)Finish Options On Every Quote
Compare finishes on your own part
Upload your CAD file and switch between mill finish, zinc plating, e-coating and powder coating to see the price and compatibility check for your exact material, geometry and part size.
Frequently Asked Questions
What is the most common surface finish for sheet metal parts?
Powder coating. According to the Powder Coating Institute, it accounts for more than 15% of the industrial finishing market. It is also the only finish here that covers aluminum, carbon steel, and stainless steel with a full color range. For indoor steel that doesn't need color, zinc plating is usually the better functional choice.
Does powder coating affect part tolerances?
Yes. Powder coating a surface makes it slightly thicker and can tighten hole diameters by 0.14 to 0.30 mm, which can be enough to exceed their tolerances. To make up for this, designers can make the holes larger, mask critical features, or factor the thickness of the coating into the drawing.
What is the difference between zinc plating and galvanizing?
Both use zinc to protect steel, but by different processes. Zinc plating electrodeposits a 5-25 µm layer, enough for indoor parts and fasteners. Hot-dip galvanizing submerges the part in molten zinc for a 50-200 µm alloyed coating suited to outdoor structural steel. Pre-galvanized sheet (SGCC) is coated at the mill, so laser cutting leaves bare edges.
Can stainless steel be powder coated?
Yes, but it needs to be pretreated first. However, stainless steel is usually specified because of its inherent corrosion resistance and appearance. Passivating the steel or giving it a brushed finish preserves both of those features and will cost less than coating it. The main reason to powder coat stainless steel is to achieve a specific color.
What are the two main types of surface finishes?
Additive finishes and conversion finishes. Additive finishes deposit material onto the part: powder coating, e-coating, zinc plating, and galvanizing. Conversion or subtractive finishes transform the metal's own surface: brushing removes metal, anodizing converts aluminum to oxide, and passivation removes free iron from stainless steel. Mill finish and antirust oiling fall outside either category, since they don't change the surface.
Which metal finish lasts longest outdoors?
It depends on the material. For carbon steel sheet metal parts, it's an e-coat primer with a powder coat on top; powder alone is rated 480-1,000h NSS on the Boda platform. For structural steel (where the appearance doesn't matter), the American Galvanizers Association rates hot-dip galvanizing as the zinc coating with the longest life.